Category Archives: Waterjet & Laser

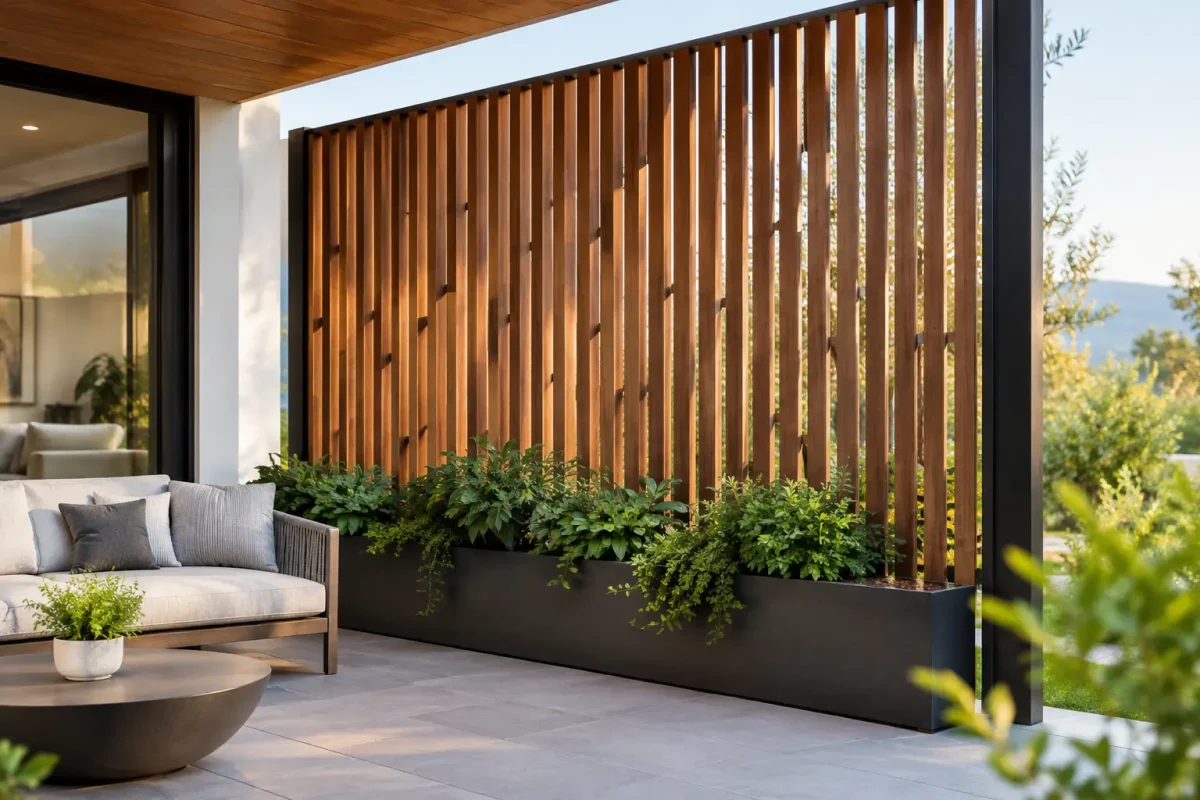
Architectural Screen Ideas That Work Harder

Architectural Screen Ideas That Work Harder

A screen can look exceptional in a project photo and still fail on site. It may block too much airflow, cast unwanted shadows, rattle in the wind or leave a private courtyard visible from the street. The best architectural screen ideas begin with the working requirement, then use pattern, material and precise cutting to meet it.

For builders, architects, fabricators and design-led property owners, a custom screen is not simply decoration. It can manage views, create a safer boundary, conceal plant equipment, divide outdoor zones or give a plain facade a considered identity. Getting those outcomes right means making a few decisions before choosing a pattern.

Start with what the screen needs to do

Privacy is often the first brief, but it needs defining. Privacy from a standing neighbour, passing footpath traffic or overlooking from an upper storey each calls for a different screen height, opening size and location. A dense pattern at eye level may be enough, while the upper portion can remain more open to protect daylight and airflow.

Shade is equally specific. A west-facing screen in Adelaide has a much tougher job than a decorative divider beneath a covered alfresco. Consider the direction of afternoon sun, whether the screen is fixed or moveable, and how the pattern will project shadows into the space. Small apertures provide stronger screening but can make a compact area feel enclosed. Larger cut-outs feel lighter, but offer less visual protection.

For commercial and industrial sites, screening may need to hide bins, pumps, air-conditioning units or service yards without restricting access for maintenance. In that setting, panel layout, gate clearances and replacement practicality matter as much as the visual finish.

Architectural screen ideas by application

A screen design works best when it relates to the surrounding architecture rather than competing with it. Clean modern buildings generally suit repeated geometry, linear cut-outs or restrained perforation. Heritage-inspired homes can carry more detailed botanical, Art Deco or lattice-based motifs, provided the pattern is not so fine that it becomes visually busy from a distance.

Entry screens that create a clear arrival

A front boundary screen can establish privacy without building a solid wall. Vertical slots create a crisp, contemporary effect and visually increase height. Offset rectangles soften the repetition while retaining a structured appearance. For a more organic result, a leaf, branch or flowing line pattern can reference garden planting and allow the screen to become a focal point.

Think about what sits behind it. A strongly patterned panel needs enough setback from a front door, garden or facade to be read clearly. When it is installed directly against another surface, the pattern can lose definition and collect debris in tight spaces.

Courtyard and pool screening

Courtyards benefit from panels that filter rather than completely block the outlook. Patterns with a gradual change in density are useful here: a tighter lower section helps with privacy, while larger openings above keep the space connected to sky and trees.

Around pools, material selection becomes more demanding. Chlorine exposure, coastal air and continual wet-dry cycles can shorten the life of poorly specified steel. Aluminium and suitable grades of stainless steel are common choices, but the finish, fixings and supporting frame must also suit the environment. A screen panel is only as durable as the least durable component in the assembly.

Balconies, facades and carports

Facade screens can reduce glare and create a stronger building identity, but they must be engineered for wind load, fixing points and panel movement. Large metal panels expand and contract with temperature changes. Allowing for that movement prevents buckling and noisy contact against the frame.

For carports and side passages, screens can obscure stored items and create a more finished street presentation. A practical design should still permit ventilation and allow room to clean behind the panels. Screens used near vehicle access also need careful placement so they do not reduce sightlines at driveways.

Choose a pattern at the right scale

The most common design mistake is selecting a pattern from a small sample without considering the finished panel size. A motif that looks refined on an A4 sheet can appear sparse over a 2.4-metre panel. Conversely, highly detailed linework may read as visual clutter once repeated across a long boundary.

View the design at three distances: close up, from the main approach and from across the street or courtyard. At close range, people notice cut quality, sharp internal corners and the consistency of narrow bridges between openings. From further away, they see the overall balance of solid material and open area.

The width of those bridges is not merely an aesthetic choice. It affects panel strength, handling and fabrication. Very narrow sections can distort during cutting, transport or powder coating, particularly in thin material. A cutting provider can help revise fine details while preserving the character of the design.

Patterns also need enough solid perimeter for mounting. If cut-outs run too close to an edge, there may be insufficient material for folds, brackets or concealed fixings. Resolve mounting early rather than trimming a finished design to make it fit.

Material and finish decisions that last

The right material depends on location, desired appearance, budget and fabrication requirements. Mild steel is economical and strong, and can be painted or powder coated for a wide range of colours. It needs an appropriate protective coating system, particularly outdoors, and any damage to that coating should be repaired promptly.

Aluminium is lightweight, corrosion resistant and well suited to many exterior installations. It is useful where lifting large panels is a concern or where a structure has limited load capacity. Its lower stiffness compared with steel may require thicker sheet, closer support spacing or a formed return edge.

Stainless steel offers excellent corrosion resistance and a premium architectural appearance. Brushed finishes can suit contemporary settings, while polished surfaces can be visually striking but show fingerprints and surrounding reflections more readily. The stainless grade should suit the exposure, especially near the coast.

Corten-style weathering steel delivers a rich, earthy surface once it develops its protective patina. It is not a fit-and-forget choice. Early runoff can stain paving, walls and nearby surfaces, so drainage detailing and the material beneath the screen need careful consideration.

Powder coating provides colour consistency and protection, but preparation matters. Laser-cut edges, welds, folded returns and any sharp corners should be properly prepared before coating. A good-looking finish starts with accurately cut, clean material.

Laser cutting or waterjet cutting?

Cutting method affects edge quality, speed, material suitability and the level of detail that can be achieved. High-definition laser cutting is an efficient choice for many steel, stainless steel and aluminium screen designs. It produces accurate profiles and clean detail quickly, making it well suited to repeated panels and production work.

Waterjet cutting uses a high-pressure stream, up to 60,000 PSI, to cut without creating a heat-affected zone. That cold-cut process is valuable when heat distortion, edge hardening or material change is a concern. It also provides versatility across materials that are not suitable for laser cutting, including stone, tile and certain composite materials.

There is no universal winner. A straightforward aluminium geometric screen may favour laser cutting for speed and economy. A detailed stainless component where heat must be avoided, or a mixed-material feature, may suit waterjet cutting. The best process is the one that protects the material and meets the finished specification.

For custom projects in Adelaide, Waterjet & Laser SA can assess the design, material and intended finish before cutting begins. That discussion can prevent avoidable issues such as undersized details, impractical fixing zones or a pattern that does not scale correctly to the panel.

Detail the installation, not just the panel

A precise screen still needs a practical installation plan. Decide whether panels will be fixed between posts, face-fixed to a frame, folded into a cassette, mounted on stand-offs or used as sliding gates. Each option changes the visible edge treatment and the amount of material required around the perimeter.

Allow drainage at the bottom of exterior screens so water and leaf litter do not sit against the panel. Specify compatible fasteners to reduce the risk of corrosion between dissimilar metals. Where screens are mounted near walls, use enough clearance for cleaning and airflow, particularly in shaded areas where moisture lingers.

If a design includes several panels, plan the joins deliberately. A continuous pattern can look impressive across a long run, but alignment tolerances, post positions and access for installation need to be built into the drawing. Sometimes a repeated modular panel produces a cleaner, more economical result and makes future replacement simpler.

The strongest architectural screen is one that earns its place every day: it gives the right amount of privacy, handles the local conditions, installs without compromise and still looks intentional years after the project is finished.

Can Laser Cut Galvanised Steel? What to Know

Can Laser Cut Galvanised Steel? What to Know

A sheet of galvanised steel can look straightforward until it reaches the cutting stage. The steel itself is familiar territory, but its protective zinc coating changes the conversation. So, can laser cut galvanised steel? Yes, with the right equipment, extraction, settings and an honest assessment of what the finished edge needs to do.

For fabrication, building, engineering and architectural work, laser cutting can be an efficient way to produce accurate profiles in galvanised sheet. It is not automatically the best process for every job, though. The zinc coating, material thickness, part geometry and required corrosion protection after cutting all need to be considered before production begins.

Can laser cut galvanised steel safely?

A high-definition CNC laser can cut galvanised steel, including common pre-galvanised sheet products, provided the machine is set up for the material and the cutting area has effective fume extraction. During laser cutting, the zinc coating at and near the cut line is heated rapidly. Zinc vapour and metal fumes are produced, so proper ventilation and filtration are essential for operator safety and for keeping the cutting system performing as it should.

This is not a material to cut casually in an unventilated workshop. Professional laser cutting operations use extraction systems designed to remove fumes at the source. The condition of the sheet matters as well. Galvanised steel that is oily, contaminated, painted or carrying an unknown coating should be identified before cutting, rather than treated as standard mild steel.

For customers, the practical takeaway is simple: specify that the material is galvanised when requesting a quote. That lets the cutting team select the appropriate process, plan safe production and advise on the likely finish around the cut edge.

What happens to the zinc coating at the cut edge?

Laser cutting creates a narrow heat-affected zone. The cut is highly localised, particularly compared with broader thermal processes, but the zinc coating immediately beside the cut will be altered or removed. The exposed steel edge will therefore not have the same continuous galvanised protection as the untouched faces of the sheet.

Whether that matters depends on the part’s application. An internal bracket used in a dry environment may need no additional treatment. A component going into outdoor construction, agricultural equipment, coastal work or a wet industrial setting may need the edges protected after cutting. Zinc-rich coatings, suitable primers, paint systems or further galvanising can be considered according to the required service life and finish.

This is often where a drawing and a short conversation save time. A decorative panel may prioritise a crisp profile and a prepared surface for powder coating. A flashing, tray or external bracket may prioritise corrosion resistance at every exposed edge. The same sheet can require a different cutting and finishing plan depending on where the finished part will be used.

When laser cutting is the right choice

Laser cutting is particularly effective when a project needs speed, repeatable dimensions and clean detail in sheet material. It is well suited to production runs of brackets, covers, gussets, mounting plates, folded-component blanks, screens and custom profiles. CNC programming also makes it practical to repeat a proven design without relying on manual marking and cutting.

For thinner galvanised sheet, laser cutting can produce narrow kerfs and accurate internal features. Holes, slots, tabs and complex external profiles can be cut directly from a digital file, reducing secondary work. The result is a blank that is ready for folding, welding, assembly or finishing, subject to the tolerances and edge condition required by the job.

It is also a strong option where turnaround matters. For Adelaide fabricators and builders managing tight programme dates, outsourced laser capacity can remove a bottleneck without the cost of buying, operating and maintaining specialised machinery in-house.

Laser cutting is not only for large production work. It can be equally useful for prototype parts, one-off replacement components and custom design pieces, particularly where the profile needs more accuracy than a hand-cut process can consistently provide.

Thickness, features and tolerances matter

There is no single answer for every gauge of galvanised steel. Material thickness influences cutting speed, edge finish and the amount of heat introduced into the part. Very thin sheet can distort if a part has long unsupported sections or fine, narrow features. Thicker plate can be cut, but the best process depends on the machine capability, the required edge condition and the complexity of the design.

Part design also matters. Small holes in relation to material thickness, tight corners, closely spaced cuts and delicate tabs can all affect how a component cuts and handles after it is removed from the sheet. Good nesting and sensible tolerances help achieve reliable results while minimising waste.

If a part will be folded after cutting, bend lines should be considered early. Keeping critical features a sensible distance from bends reduces the risk of distortion and gives the fabricator more room to work. Providing a clear DXF, DWG or dimensioned drawing, together with material grade, thickness and quantity, helps turn a quote into a production-ready job.

Where waterjet cutting may be the better option

Laser is fast and precise, but it is a thermal process. When heat must be avoided entirely, CNC waterjet cutting offers a useful alternative. Waterjet cuts with a high-pressure stream of water and abrasive, rather than a laser beam, so it does not create a heat-affected zone or heat distortion in the material.

That makes waterjet worth considering for parts where preserving the galvanised coating close to the cut edge is especially valuable, where the design contains heat-sensitive detail, or where material flatness is critical. It can also be a practical choice for thicker material and for projects that combine galvanised steel with other materials.

The trade-off is that waterjet cutting is typically slower than laser cutting in thin sheet, and the cut edge has a different appearance. Neither process is universally superior. The right choice comes down to the material, thickness, required quantity, edge specification, timeframe and budget.

Waterjet & Laser SA can assess both options onsite, rather than trying to force every profile through a single process. That capability gives customers a clearer path to the outcome they actually need: accurate parts, suitable edge quality and dependable delivery.

How to prepare a galvanised steel cutting job

The most useful information is usually straightforward. State whether the sheet is pre-galvanised or already fabricated, nominate the thickness and provide the required quantity. Include the finished use of the part where corrosion protection, visual appearance or tight tolerances are important.

It also helps to identify any downstream process. Will the part be folded, welded, painted, powder coated or left raw? Will it be installed outdoors, exposed to salt air or used in a clean internal environment? These details affect recommendations around cut direction, edge cleanup and post-cut protection.

If you are supplying material, ensure it is flat, clean and clearly identified. If the steel has a coating beyond standard galvanising, such as paint, plastic film or adhesive residue, mention it before production. Assumptions around coatings can create avoidable delays and may affect the selected cutting method.

For larger runs, a first-off sample can be worthwhile when the part has critical fit-up requirements. It confirms hole sizes, slot clearances, bend allowances and the visual quality of the edge before the full batch is cut. That is particularly valuable for fabricated assemblies where a minor dimensional issue can slow work across multiple components.

The practical decision for your next job

Laser cutting galvanised steel is a proven, capable option when the work is managed correctly. The key is not simply whether the laser can pierce the sheet. It is whether laser cutting delivers the right combination of speed, profile accuracy, edge condition and corrosion performance for the finished component.

If the job needs rapid, repeatable profiles in galvanised sheet, laser cutting may be the efficient answer. If heat-free cutting and maximum material integrity around the cut are the priority, waterjet may be the stronger fit. Bringing those requirements into the conversation before the sheet is loaded is the best way to keep parts accurate, protect the finish where it matters and keep fabrication moving.

Mining Wear Plate Cut for Accurate Fabrication

Mining Wear Plate Cut for Accurate Fabrication

A mining wear plate can be the difference between a planned maintenance stop and an expensive shutdown. When a chute liner, hopper wall or excavator component arrives with holes out of position, a poor edge, or heat-affected distortion, the cost is not limited to the part. Fitters lose time, fabrication crews start reworking, and equipment remains out of service longer than it should.

Wear-resistant plate is specified to take punishment. Cutting it accurately without compromising the design calls for the same practical thinking. Material grade, thickness, profile complexity, hole size, edge requirements and delivery timing all affect the best cutting approach.

What makes mining wear plate different?

Mining wear plate is built for abrasive environments where ordinary mild steel wears away too quickly. It is commonly used in liners, bins, chutes, hoppers, transfer points, crushers, screens, buckets and material-handling equipment. Depending on the application, the plate may need to resist sliding abrasion, impact, gouging or a combination of all three.

Many wear plates are high-hardness steels, often supplied with a hardened surface or hardened through the plate. That hardness is valuable in service, but it changes the fabrication conversation. The material is less forgiving than standard structural steel, and careless cutting, forming or welding can introduce avoidable problems.

A good profile-cut part should arrive ready for the next operation with dimensions that match the drawing, clean features where they matter, and an edge condition suited to the component’s job. There is no value in selecting premium wear plate only to lose time correcting a cut profile on the workshop floor.

Start with the operating conditions, not just the grade

Plate selection should reflect what is actually wearing the component. Fine, dry ore sliding continuously across a chute behaves differently from oversized rock impacting a loader bucket. A liner exposed to wet slurry may require a different balance of wear resistance, corrosion behaviour and replaceability than a dry crushing plant application.

Harder is not automatically better. Very high hardness can improve abrasion resistance, but it may also affect fabrication options and make certain designs less practical. Plate thickness adds service life in some applications, yet it also adds weight, affects handling and may alter the way a component is supported.

For replacement liners, the existing part is useful evidence. Look at where wear is concentrated, whether the plate has cracked near bolt holes, and whether the component is wearing evenly. Those details can indicate that the issue is not simply plate life. Hole placement, liner segmentation, backing support, material flow or installation method may need attention too.

Cutting mining wear plate without creating extra work

The cutting method should be chosen around the material and the finished-part requirement. In a production environment, speed matters, but so do dimensional control and material integrity.

Waterjet cutting for cold-cut precision

CNC abrasive waterjet cutting uses a high-pressure stream of water and abrasive to cut through material without introducing a heat-affected zone. At pressures up to 60,000 PSI, waterjet technology can accurately profile hard plate, including detailed shapes, internal cut-outs and bolt-hole patterns.

For wear plate, the cold-cut process is particularly useful where preserving the plate’s properties near the cut edge is a priority. There is no thermal distortion from the cutting process, no heat-induced hardening at the edge, and no need to allow for a conventional heat-affected zone. This can make waterjet a strong option for intricate liners, tight nesting requirements and components with features close to an edge.

The trade-off is that waterjet may not be the fastest or most economical choice for every simple, high-volume profile. Cut time varies with thickness, material hardness, tolerances and the amount of internal detail. For the right job, however, the accuracy and clean cold-cut result can remove downstream work and protect the value of the material.

Laser cutting where speed suits the job

High-definition laser cutting can be an efficient solution for suitable wear plate grades and thicknesses, particularly when parts are straightforward and turnaround is critical. It can produce clean, accurate profiles at speed and is well suited to repeatable production work.

Because laser cutting is a thermal process, the edge condition and heat input must be considered. For some components, this is entirely acceptable. For others, especially where the material manufacturer’s fabrication guidance is strict or where edge performance is critical, cold-cut waterjet processing may be the better fit.

The practical answer is not to choose a process by habit. Assess the drawing, plate specification and intended service. Having both laser and waterjet capability available means the cutting method can be matched to the part rather than forcing every job through the same machine.

Details that prevent fit-up delays

Most wear-plate problems are not caused by the outside profile alone. They appear at the points where the part must locate, bolt on, weld in or sit against another component.

Bolt holes need particular attention. Their diameter, tolerance, counterbore requirements and relationship to the plate edge all affect installation. If a liner needs to be replaced inside a confined chute during a shutdown, a hole pattern that allows practical alignment can be as valuable as an extra increment of wear resistance.

Internal corners are another common issue. A sharp inside corner can concentrate stress and may be difficult to produce exactly as drawn, depending on the cutting process. Adding an appropriate radius can improve manufacturability and reduce the chance of cracking in a highly loaded part. The required radius depends on the design and process, so it is worth discussing before production begins.

Where a part will be welded, allow for the welding procedure and the plate supplier’s recommendations. Some wear-resistant grades require controlled preheat, consumable selection or other precautions. Accurate profile cutting supports a better weld fit-up, but it does not replace sound welding practice.

Give the cutter information that matters

A clear drawing saves time at quoting, programming and fabrication stages. It also reduces the risk of assumptions being made on critical details. Along with the part dimensions, provide the material grade, thickness, quantity, required tolerances and any features that must be held especially accurately.

For more complex mining components, include the following information:

  • Whether the plate is supplied by the customer or needs to be sourced.
  • Which face is the wear face, where that affects marking or orientation.
  • Hole sizes, thread preparation requirements and whether holes are for bolts, plugs or locating pins.
  • Edge expectations, such as whether a cut edge will be exposed, welded, machined or used as a mating surface.
  • Required delivery date and whether the parts need to be labelled, nested in sets or packed for a site shutdown.

A DXF file is often the most efficient format for CNC profile cutting, while a dimensioned PDF can assist with checks and material notes. If only an existing liner or sample is available, it may still be possible to work from a measured part, but confirming critical dimensions before cutting is essential.

Think beyond the individual plate

The best outcome is not always one large, heavy liner. In some situations, breaking a liner into manageable sections can simplify handling, reduce change-out time and allow the highest-wear areas to be replaced independently. More joints and fasteners may add complexity, so the decision depends on access, lifting capacity, wear pattern and maintenance planning.

Nesting is also worth considering. Efficiently arranging parts on a sheet can reduce waste, especially when the job includes multiple liner shapes or repeat components. A cutting partner can help review whether a small design adjustment improves yield without affecting performance.

For Adelaide and South Australian mining support businesses, local cutting capacity can be particularly valuable when a shutdown date is fixed and freight time is tight. Fast response should still include proper drawing review, material confirmation and a process choice that makes sense for the component.

Waterjet & Laser SA combines CNC waterjet and laser cutting so fabricators can select the process that suits the material, edge requirement and program timing. The goal is simple: accurate parts that move into fabrication with less rework and greater confidence.

Before the next liner replacement or repair package is released, review the parts that caused the most trouble last time. A better hole pattern, a more practical segmentation plan or the right cold-cut process may be the small change that keeps the shutdown on schedule.

Waterjet vs Plasma for Aluminium Compared

Waterjet vs Plasma for Aluminium Compared

A warped aluminium bracket, a rough edge that needs grinding, or holes that have closed up after cutting can quickly turn an economical job into a costly delay. When comparing waterjet vs plasma for aluminium, the right process comes down to more than getting through the material. It affects fit-up, finishing time, part accuracy and how the aluminium performs in the next stage of fabrication.

Plasma is a fast, capable process for many conductive-metal jobs. Waterjet cutting takes a different approach, using a high-pressure stream of water and abrasive to cut without heat. For aluminium parts where edge condition, detail and material integrity matter, that difference is significant.

How plasma cutting handles aluminium

Plasma cutting uses an electrically conductive gas arc to melt metal, while a high-velocity gas stream removes the molten material from the cut. Aluminium is conductive, so plasma can cut it efficiently, particularly where production speed matters more than a fine finished edge.

For thicker plate, structural components and parts that will be welded, machined or ground after cutting, plasma can be a practical choice. It is generally faster than abrasive waterjet cutting on many aluminium thicknesses and can offer a lower cutting cost when tolerances are less demanding.

The trade-off is heat. Aluminium conducts heat extremely well, yet thin sheet and narrow features can still be affected by the concentrated thermal input of plasma. The cut edge can show a heat-affected zone, dross or oxide residue, and some parts may require secondary clean-up before fabrication or finishing.

Plasma cut quality also varies with material thickness, machine set-up, consumable condition and travel speed. A good operator and high-definition plasma system can produce useful results, but plasma is not usually the first choice for intricate profiles, tight internal corners or parts that need to come off the table ready for a visible finished application.

Waterjet vs plasma for aluminium: the key differences

The most useful comparison is not which method is universally better. It is which process reduces work and risk for your particular part.

Heat and material distortion

Waterjet is a cold-cut process. At pressures up to 60,000 PSI, the waterjet stream and abrasive cut through aluminium by erosion rather than melting. There is no heat-affected zone and no heat distortion caused by the cutting process.

That matters for thin aluminium sheet, close-tolerance parts, machined components and panels with detailed internal cut-outs. It also helps where flatness is important, such as covers, facias, architectural pieces and components that must sit cleanly against another surface.

Plasma introduces heat as part of the process. On a simple heavy plate profile, this may be acceptable. On lighter gauge aluminium or closely spaced features, it can create movement that needs to be corrected, or dimensions that need additional finishing work.

Edge quality and finishing work

A waterjet-cut aluminium edge is typically clean, square and free from thermal discolouration. The cut may have fine striations, depending on the required speed and quality setting, but it does not carry the hardened or heat-altered edge associated with thermal cutting.

This can remove steps from the job. If a part is heading to powder coating, anodising, assembly or a visible architectural installation, less grinding and edge dressing can mean a more consistent final result. Waterjet is also well suited to aluminium parts that need accurate slots, tabs, holes and interlocking profiles.

Plasma edges can be entirely suitable when the part will be welded, ground, painted or otherwise processed later. However, dross removal and edge clean-up should be allowed for in the production plan. If every part needs hand finishing before it can move forward, the initial speed advantage can narrow quickly.

Accuracy and design detail

Waterjet cutting is the stronger option for complex geometry. Fine internal shapes, tight radii, small holes, decorative patterns and detailed nested parts can be cut accurately without creating a large heat zone around the profile.

For fabricators, this supports better fit-up and repeatability. For designers and builders, it allows more freedom in aluminium screens, signage, feature panels and custom components where every line is visible. Waterjet can also cut material without needing a heat-sensitive protective process around the edge.

Plasma is more suited to larger, simpler profiles. It can handle circles, brackets, gussets and general plate shapes effectively, but kerf width, taper and thermal effects make it less appropriate where fine detail and close tolerances are central to the brief.

Thickness and cutting speed

Plasma’s main advantage is speed. On suitable aluminium plate, especially when parts are straightforward and a secondary operation is already expected, plasma can be an efficient production process.

Waterjet is usually slower, particularly in thicker materials and when a high-quality edge finish is specified. That slower cutting time needs to be weighed against the time saved in deburring, straightening, machining or remaking distorted parts. The best value is the finished part cost, not simply the machine cutting rate.

Waterjet also offers broad thickness capability and maintains its cold-cut benefits across a wide range of aluminium jobs. The practical limit will depend on the grade, thickness, profile detail and tolerance required, so it is worth reviewing the drawing before locking in a process.

Waste, safety and downstream work

Both methods can be programmed efficiently to nest parts and reduce material waste. Their workshop impacts differ, however. Plasma creates bright arc light, fumes and molten material, requiring suitable extraction and safety controls. It is an established process, but it is inherently thermal.

Waterjet produces no heat-affected zone, fumes or thermal distortion in the workpiece. The process uses water and abrasive garnet, with the spent material managed through the cutting system. For aluminium components that need clean handling and minimal alteration before the next operation, this is a useful advantage.

When plasma is the sensible choice

Plasma is not a poor choice for aluminium. It is often the sensible choice when the job involves simple profiles, moderate tolerances and sufficient thickness to make fast cutting valuable. It can suit structural parts, fabrication blanks and production work where the edge will be welded, ground or machined anyway.

It is also worth considering when lead time depends on processing a high volume of uncomplicated parts quickly. In these cases, a fabricator may accept a little dross or edge preparation because it is already built into the workflow.

The key is to be realistic about the final requirement. If a plasma-cut edge needs extensive manual work to meet the drawing, the process may not be delivering the expected saving.

When waterjet is the better aluminium cutting method

Choose waterjet when the part needs to retain its original material properties right to the cut edge. It is particularly effective for thin sheet, precision components, decorative work, panels with detailed cut-outs and aluminium that will be anodised, powder coated or installed without heavy edge finishing.

It is also a strong option for prototypes and short runs. Design changes can be applied directly to the cutting file, allowing intricate profiles to be produced without dedicated tooling. For custom fabrication, this provides flexibility without compromising accuracy.

Waterjet becomes especially valuable where several requirements meet at once: a complex shape, a clean visible edge, close tolerances and no tolerance for heat distortion. That combination is where a cold-cut process can prevent problems before they reach the workshop floor.

Specify the finished result, not only the cutting method

A good aluminium cutting quote starts with the outcome you need. Provide the material grade and thickness, drawing format, quantity, critical dimensions, visible faces and any next-stage processes such as folding, welding, coating or machining. These details help determine whether speed, precision, edge finish or heat control should take priority.

For Adelaide fabricators, builders, engineers and designers, Waterjet & Laser SA can assess the drawing and recommend the cutting process that makes practical sense for the job. Bringing the finished-part requirement into the discussion early is the simplest way to avoid unnecessary clean-up, rework and hold-ups later.

Best Files for CNC Profiling in Production

Best Files for CNC Profiling in Production

A profile can be dimensionally perfect on screen yet still create delays, extra programming work or an inaccurate part on the cutting bed. Choosing the best files for CNC profiling gives your cutter clear geometry to work from, protects the intended dimensions and helps keep a job moving from quote to finished parts without avoidable rework.

For most 2D cutting work, the answer is straightforward: a clean, full-scale DXF file is usually the most dependable starting point. But the right file also depends on whether the part is being laser cut or waterjet cut, how complex the design is, and whether the drawing contains only cut paths or important fabrication information as well.

Best files for CNC profiling: start with a clean DXF

DXF is the preferred format for most CNC profiling jobs because it transfers 2D vector geometry cleanly between CAD systems and cutting software. Lines, arcs, circles and polylines remain editable mathematical entities rather than a collection of pixels. That gives the programmer a reliable basis for toolpath creation, nesting and checking dimensions before cutting begins.

A good DXF should be drawn at 1:1 scale and contain the finished part outline. If a bracket is 250 mm long, it should measure 250 drawing units in the file, not 25,000 or 0.25. Metric millimetres are generally the clearest choice for Australian fabrication work, but the units should be stated where there is any possibility of confusion.

The file extension alone does not guarantee a trouble-free job. A DXF exported from CAD software can still contain duplicate lines, open contours, broken arcs, construction geometry and layers that are not intended to be cut. Those issues are manageable, but they take time to identify and can affect price, lead time and accuracy if they are not caught early.

DWG files are also commonly supplied and can be useful, particularly when they are the original drawing. Where possible, exporting a clean DXF from the latest drawing gives the clearest result for 2D profiles. It avoids version conflicts and reduces the risk of unwanted information coming across with the file.

Vector files work. Images usually do not.

A vector file describes shape and position precisely. A raster image, such as a JPG, PNG or screenshot, describes coloured pixels. That distinction matters when a machine needs to cut a 6 mm hole, follow a complex decorative pattern or hold a critical centre distance.

PDF files can be useful when they contain true vector artwork. They are common for architectural screens, signage-style patterns and design concepts created in illustration software. However, many PDFs are simply scanned drawings or flattened images, so they may need to be redrawn before a CNC machine can use them accurately. An editable DXF remains the better production file when available.

SVG and AI files can also provide clean vector artwork for decorative work, logos and intricate shapes. Before cutting, paths may need to be converted, joined and checked for scale. This is especially relevant where a design has been prepared for print or web display, where units and line weights do not necessarily reflect real-world dimensions.

A photograph, hand sketch or image from a mobile can still be a useful reference for an early discussion. It is not normally a cutting file. If the job involves reproducing an existing part, a clear photo with measured dimensions, hole sizes and material thickness can help establish what needs to be drawn or reverse engineered.

What a production-ready profile file should contain

The best file is not necessarily the most detailed one. For CNC profiling, it should clearly show the geometry that needs cutting and separate that geometry from information intended only as a reference. A clean file allows the programmer to focus on the cutting process rather than interpreting the drawing.

Before sending a file, check these essentials:

  • All cut shapes are closed where they need to be closed, with no tiny gaps between line ends.
  • Duplicate lines, overlapping entities and hidden geometry have been removed.
  • Holes, slots, internal cut-outs and external profiles are on clear layers or distinguished by colour where required.
  • Dimensions are correct at full scale, and the drawing units are confirmed as millimetres.
  • Text, notes, dimensions and title blocks are moved to a non-cut layer or supplied in a separate PDF.

Closed geometry is particularly important. A rectangle that looks complete may actually contain four separate lines with a minute gap at one corner. A person can barely see it on screen, but CNC software sees an open path. Likewise, an imported curve made from thousands of short segments may cut differently from a smooth arc, particularly on a detailed laser-cut feature.

Where possible, use lines, arcs, circles and joined polylines instead of splines. Splines can be suitable for organic designs, but they sometimes export unpredictably between systems. Converting a spline to an appropriate polyline can improve compatibility, provided the conversion does not visibly flatten the curve or create excessive points.

Give the cutting team the information geometry cannot show

The profile file tells the machine where to cut. It does not always tell the operator what the finished part needs to achieve. A short accompanying note or PDF drawing can prevent assumptions on material, finish and quantity.

State the material grade where it matters, along with thickness, quantity and any required tolerances. Identify which face is visible if cosmetic edge appearance, protective film or grain direction is relevant. For folded, welded or assembled parts, indicate critical dimensions and whether the drawing represents the flat pattern or the finished assembly.

Also include any requirements for etching, marking, countersinks, tapped holes or post-cut fabrication. These operations are different from profiling and should not be assumed from a line colour alone. If an existing part must fit with another component, provide the mating dimensions rather than relying only on the apparent shape.

For repeat production, include a clear part number and revision. A file named “bracket final final 2” can create uncertainty when several people are involved in purchasing, fabrication and approval. A practical name such as “BRK-104 Rev C 6mm 316SS” makes it easier to trace the correct version throughout the job.

Match the file to waterjet or laser cutting

Both CNC waterjet and laser cutting rely on accurate geometry, but material behaviour and process capabilities influence how a profile is prepared. The file may be the same, while the cutting strategy differs.

Laser cutting is highly efficient for many sheet-metal profiles, particularly where speed, repeatability and fine detail are priorities. Heat is introduced into the cut zone, so the material type, thickness and feature size should be considered during quoting and programming. Very small holes, narrow webs and tight internal corners may need process-specific review.

Waterjet cutting uses a high-pressure stream, up to 60,000 PSI, to cut without a heat-affected zone. This cold-cut process is valuable for materials that can be affected by heat, including certain steels, aluminium, rubber, foam, tile, stone and layered materials. It is also well suited to thicker sections and materials beyond conventional sheet metal.

Neither process automatically makes a poor file better. A waterjet can preserve material integrity without heat distortion, while a laser can deliver fast, high-definition profiles, but both need correct dimensions and usable contours. The right cutting method depends on the material, thickness, edge requirement, tolerance, quantity and deadline.

Allow for kerf, tabs and practical cutting limits

The cutting path has width. This is known as kerf, and it varies by process, material and thickness. CNC software can apply kerf compensation so the finished part matches the required dimension, but the drawing must represent the intended finished geometry rather than an assumed cutter centreline.

In nested sheet jobs, small parts may need tabs or a holding strategy so they remain stable during cutting. This is especially relevant for fine laser-cut work and intricate decorative designs. If a visible edge must remain completely clean, say so early. The programmer can then choose a suitable method rather than treating all edges the same.

Tight internal corners also have a practical limit. Waterjet and laser cutters follow a path with a finite kerf, so a perfectly sharp internal corner cannot always be produced exactly as drawn. If a square corner must receive a mating part, a small relief feature may be required. This is a design decision worth addressing before material is on the bed.

Send the clearest version, not every version

When a job is ready for quote or production, send the editable profile file together with a PDF for visual confirmation. The DXF provides the geometry; the PDF shows the intended orientation, notes and critical dimensions. This combination reduces the chance that a clean-looking profile is cut upside down, at the wrong revision or without an important non-cut requirement.

For Adelaide fabricators, builders, designers and manufacturers working to a short programme, this preparation is often the difference between a quick release to cutting and a chain of clarification emails. Waterjet & Laser SA can review supplied files and help identify practical issues before cutting, particularly where a design is complex or the material calls for a particular process.

The strongest file is simply one that leaves nothing critical to guesswork: clean 1:1 geometry, confirmed material details and a clear statement of what the finished part must do. That gives your cutting partner the best chance to deliver accurate parts first time, ready for the next stage of fabrication.

Secret Link