Category Archives: Waterjet & Laser

Choosing Custom Gasket Materials for Demanding Jobs

Choosing Custom Gasket Materials for Demanding Jobs

A gasket can be a small component with a large consequence. When it is cut from the wrong material, sized inaccurately or damaged at the edge, the result may be a leak, pressure loss, contamination, vibration, premature wear or unplanned downtime. Choosing custom gasket materials is therefore not simply a matter of matching thickness and tracing a shape. It is about selecting a material that will keep sealing under the actual conditions of the job.

For fabricators, maintenance teams, builders and manufacturers, a custom-cut gasket can remove the compromises that come with modifying an off-the-shelf part. The right material and cutting method help produce a clean, accurate profile that fits first time and performs as intended.

Start With the Conditions the Gasket Must Handle

Every gasket selection should begin with the operating environment. A material that performs well in a dry, low-pressure enclosure may fail quickly in a pump, flange, exhaust assembly or chemical-processing application. Temperature, pressure, media, surface condition and bolt load all influence the material choice.

Consider what will contact the gasket. Water, oil, fuel, air, steam, coolant, abrasive slurry and cleaning chemicals all affect materials differently. Nitrile rubber, for example, is commonly selected where oil resistance is required, while EPDM can suit water, weathering and many outdoor applications. Silicone is often useful across a broad temperature range, while specialised high-temperature materials may be required around exhausts, heaters and industrial equipment.

The pressure involved matters just as much. Higher pressure can force softer materials out from between mating faces, particularly where flange gaps are uneven or fasteners are not tightened consistently. In these situations, a denser or reinforced sheet material may be the better option. The ideal choice depends on the full assembly, not just the fluid being sealed.

Custom Gasket Materials Need the Right Balance

There is rarely one universally best gasket material. The best option is the one that balances sealing performance, service life, availability and cost for the specific application.

Soft rubber and foam materials can conform well to irregular surfaces and are often effective for dust seals, weather seals, access panels, acoustic isolation and low-pressure enclosures. Their flexibility can be an advantage, but they may not suit high heat, harsh chemicals or heavily loaded joints.

Fibre, cork-rubber and compressed sheet products are frequently used where mechanical strength and fluid resistance are both needed. These materials can be suitable for machinery covers, automotive components, pumps and general industrial sealing, provided the selected grade matches the temperature and chemical exposure.

For more demanding applications, engineers may specify PTFE, graphite-based products, mica, specialist high-temperature composites or reinforced gasket sheet. These choices can offer excellent chemical or thermal resistance, but may require closer control of flange finish, bolt loading and gasket thickness. Higher-performing material is not automatically the most cost-effective answer if the application does not require it.

Thickness is another trade-off. A thicker gasket can accommodate minor variation in mating surfaces, but excessive thickness can reduce stability, increase compression set or create problems under pressure. A thinner gasket can provide a more controlled seal where surfaces are flat and accurately machined. Good advice starts with understanding the joint, rather than selecting a thickness by habit.

Why Precision Cutting Changes Gasket Performance

Material selection is only half the job. A gasket must also be cut accurately enough to match bolt holes, ports, internal openings and outside dimensions. Even a suitable material can fail if a port is partially obstructed, a hole is out of position or the part is stretched and distorted during cutting.

CNC waterjet cutting is particularly effective for many custom gasket materials because it is a cold-cut process. The cutting stream does not introduce a heat-affected zone, which helps preserve the material properties of rubbers, foam, cork, fibre sheet and other heat-sensitive materials. There is no melted edge to harden, shrink or create an inconsistent sealing face.

Waterjet cutting also allows intricate profiles to be produced directly from a drawing, sample or supplied dimensions. This is valuable for replacement gaskets where original parts are worn, discontinued or unavailable. With the right source information, a profile can be recreated for a one-off repair or repeated as a production run.

Laser cutting can be an efficient option for selected gasket materials, particularly where the material responds cleanly to heat and high-volume repeatability is required. However, some elastomers and soft materials can char, melt or develop an altered edge under laser heat. The best cutting process depends on the material grade, thickness, tolerances and finish required. An experienced cutting provider will assess that before production begins.

Drawings, Samples and Tolerances Matter

A clean DXF file is often the quickest route to a precision-cut gasket, especially for a repeat job. It defines the outside profile, internal cut-outs, bolt pattern and key dimensions clearly. But a formal drawing is not the only starting point.

A physical sample can be useful when replacing an existing gasket, provided it has not stretched, torn or compressed excessively in service. Measurements can then be checked against the mating component where possible. Photographs, hand sketches and critical dimensions can also assist with straightforward shapes, although accuracy improves when the sealing faces or original CAD information are available.

Tolerances should suit the job. A large access-panel seal does not require the same level of control as a gasket with closely spaced ports or small mounting holes. Specifying unnecessarily tight tolerances can add cost without improving performance. On the other hand, tolerances that are too loose can create alignment issues and sealing failures. Clear communication about the working function of the part helps determine what is practical.

Avoid Common Gasket Specification Mistakes

The most common mistake is selecting a material based only on what was used previously. A replacement gasket may look similar, but the equipment could now be running hotter, using a different fluid or operating at higher pressure. The original material may also have been a compromise rather than the best available choice.

Another issue is overlooking compression. A gasket is designed to be compressed, but not crushed beyond its useful range. The fastener pattern, torque procedure, flange flatness and gasket hardness all work together. If the material is too soft, it may creep over time. If it is too hard, it may not conform sufficiently to seal small imperfections.

Edge quality should not be treated as cosmetic. Rough edges, heat damage, loose fibres or poorly formed holes can interfere with fitment and create potential leak paths. This is especially relevant for thin material, intricate geometries and components exposed to pressure or fluid flow.

Finally, do not forget the practical details: quantity, nesting requirements, identification, packing and delivery timing. A maintenance shutdown may need a single urgent replacement, while a production line may require hundreds of identical parts supplied in a controlled, repeatable format.

Local Cutting Support for Gasket Projects

For Adelaide and South Australian customers, local cutting capacity can make a real difference when parts are urgent or material needs to be assessed before cutting. Waterjet & Laser SA combines onsite CNC waterjet and laser cutting to match the process to the material and the job requirements.

Whether the requirement is a simple rubber strip, a complex machinery gasket, a foam seal or a repeat batch of profile-cut sheet material, the aim is the same: accurate parts, clean handling and dependable turnaround. Supplying the material type, thickness, operating conditions, quantity and a drawing or sample early in the process gives the cutting team the information needed to produce the right result.

A gasket should not be the weakest link in an otherwise well-built assembly. Select the material for the conditions it will actually face, then have it cut with the accuracy the application deserves.

Ordering Profile Cut Parts Without Rework

Ordering Profile Cut Parts Without Rework

A profile cutting job can look straightforward on screen, then become costly on the workshop floor. A hole that is a fraction undersize, a bend allowance overlooked, or the wrong process selected can hold up fitting, welding and installation. Ordering profile cut parts successfully comes down to providing the right information before material reaches the cutting bed.

For fabricators, builders, engineers and designers, outsourced cutting should reduce workload, not create another inspection and correction step. Clear drawings, realistic tolerances and an early conversation about the part’s purpose help deliver components that arrive ready for the next operation.

Start ordering profile cut parts with the end use

The best drawing is not always the one with the most dimensions. It is the one that clearly communicates what the finished part must do. A gusset for a structural frame, a stainless cover panel, a rubber gasket and an intricate architectural screen may all be profile cut parts, but they have very different requirements for edge finish, material condition, hole detail and cutting method.

Before requesting a quote, consider how the component will be used after cutting. Will it be welded, folded, machined, powder coated, polished, bolted into an existing assembly or installed as a visible finished feature? This context affects sensible tolerances and whether minor cut marks, edge taper or heat effects matter to the job.

For example, a decorative aluminium panel may need clean visual edges and carefully placed micro-joints so parts can be removed without marking the face. A steel bracket intended for welding may prioritise accurate hole positions and fast production. Stating the end use prevents assumptions and gives the cutting team a practical basis for recommending waterjet or laser cutting.

Supply a drawing that can be cut accurately

A clean vector file is the quickest route from concept to production. DXF files are commonly preferred for profile cutting because they communicate geometry directly. DWG, STEP, PDF and other formats can also be useful, particularly where dimensions, notes or 3D context are needed. A PDF is often suitable for a simple one-off part, provided it is drawn to scale and includes all critical dimensions.

Avoid sending screenshots, photographs of hand sketches or image files as the only source of geometry when accuracy matters. They can be used to explain an idea, but they require interpretation and redraw time. That introduces avoidable cost and the risk of a dimension being misunderstood.

Your drawing should show the finished profile rather than tooling paths. Duplicate lines, overlapping entities, open contours and stray points can cause delays in programming, particularly on detailed patterns. If you are exporting from CAD, check that units are correct and that circles, slots and internal cut-outs are present at their intended finished size.

Where a part needs to match existing holes, posts or fabricated components, nominate the critical dimensions. It is rarely necessary to apply an extremely tight tolerance to every edge. Doing so can add cost without improving the fit. Instead, identify the dimensions that control assembly, such as hole centres, slot widths, bearing faces or the overall location of a mounting pattern.

Include the details that prevent assumptions

A quotation request is faster and more accurate when it covers four practical points:

  • material grade, thickness and whether material is customer supplied or required
  • quantity required, including whether it is a prototype, one-off or repeat production run
  • critical dimensions, tolerances and any areas that need a particular edge quality
  • required delivery date and any secondary work, such as tapping, countersinking, folding or finishing

If material is customer supplied, advise its exact grade and condition where possible. Plate that has been previously used, painted, heavily scaled, distorted or covered in protective film may need different handling. For laser cutting, reflective materials and surface condition can influence the preferred approach. For waterjet cutting, the material’s thickness and hardness influence cutting time and finish expectations.

Choose waterjet or laser based on the part

Both processes produce accurate profile cut parts, but they solve different problems. The right choice depends on material, thickness, detail, required finish and lead time.

Laser cutting is generally an efficient choice for many steel, stainless steel and aluminium jobs, particularly where parts are made from sheet and turnaround is a priority. It offers high-definition detail and repeatable profiles for brackets, panels, enclosures, machine components and fabricated assemblies. Depending on the material and specification, there may be a small heat-affected zone. For many fabrication applications this is entirely acceptable, but it should be considered where heat distortion or a changed edge condition could affect the next process.

Waterjet cutting uses a high-pressure stream of water, with abrasive added for hard materials, to cut without introducing heat into the workpiece. At pressures up to 60,000 PSI, it can produce intricate profiles in steel, stainless steel, aluminium, tile, pavers, rubber, foam, timber and many other materials. Because it is a cold-cut process, waterjet is particularly valuable for heat-sensitive materials, thicker sections, laminated products and jobs where preserving material integrity is critical.

There is no automatic winner. A simple run of thin metal brackets may be better suited to laser for speed. A detailed stainless component where heat must be avoided, or a custom gasket in rubber, may be better suited to waterjet. Having both capabilities available onsite means the process can be selected for the job rather than forcing every part through one machine.

Design features that affect cost and lead time

Small design decisions have a real effect on programming and cutting time. Very small holes in thick plate, tight internal corners, narrow webs and densely repeated detail may be achievable, but they should be assessed against material thickness and the function of the part.

An internal corner cannot be perfectly sharp when cut with a round cutting stream or laser beam. If a square internal corner is required for a mating component, a relief feature or a small radius may be necessary. This is common in tab-and-slot fabrication. Designing for the process early is usually quicker and more economical than modifying parts after the first assembly test.

Part nesting also matters. When multiple components are required from the same sheet, a cutting provider can often arrange them efficiently to reduce waste. However, the lowest material waste is not always the only priority. Part orientation, grain direction, protective film, visual finish and extraction of delicate parts can all influence the nesting strategy.

For thin or detailed components, micro-joints may be used to hold each piece in place while it is cut. They prevent small parts from tipping or moving, but they leave tiny tabs that need to be removed. If the visible face must remain pristine, say so before production. The removal method and tab location can then be planned around non-critical edges.

Check the quote before releasing production

A good quote should confirm more than a price. Read the material description, thickness, quantities and revision of the drawing carefully. If there are multiple versions of a part, make sure the file name and revision are unambiguous. A simple revision reference can prevent an old drawing being cut when changes have been made under pressure.

Also confirm whether the quoted part is cut-only or includes further work. Cutting a profile, deburring edges, removing tabs, countersinking holes and arranging delivery are separate considerations. They may all be available, but they should not be assumed.

Lead time should be discussed in relation to the actual project deadline, not just the date parts are wanted on site. Allow time for delivery, inspection, welding, coating and installation. For urgent Adelaide and South Australian projects, local production and dependable delivery coordination can remove a significant amount of uncertainty, especially when a missing component has stopped a fabrication job.

Make repeat orders easier

Once a part has been proven in the field, record the file name, material, thickness, quantity and any agreed production notes. This creates a reliable reference for repeat orders and reduces the chance of variation between batches. If a small design change is made, issue it as a new revision rather than editing the old file without notice.

For regular fabrication work, it is also worth building a small library of standard parts. Base plates, brackets, cleats, cover plates and gasket shapes can be reordered quickly when the specification is clear. That does not mean every job should be treated as standard, though. A change in material source, thickness or final use may still justify a fresh check.

Accurate cutting begins well before the machine starts. Bring a clear drawing, define what matters to the finished part, and be open about the job’s deadline and downstream processes. The result is not merely a cut shape, but a component that earns its place in the assembly.

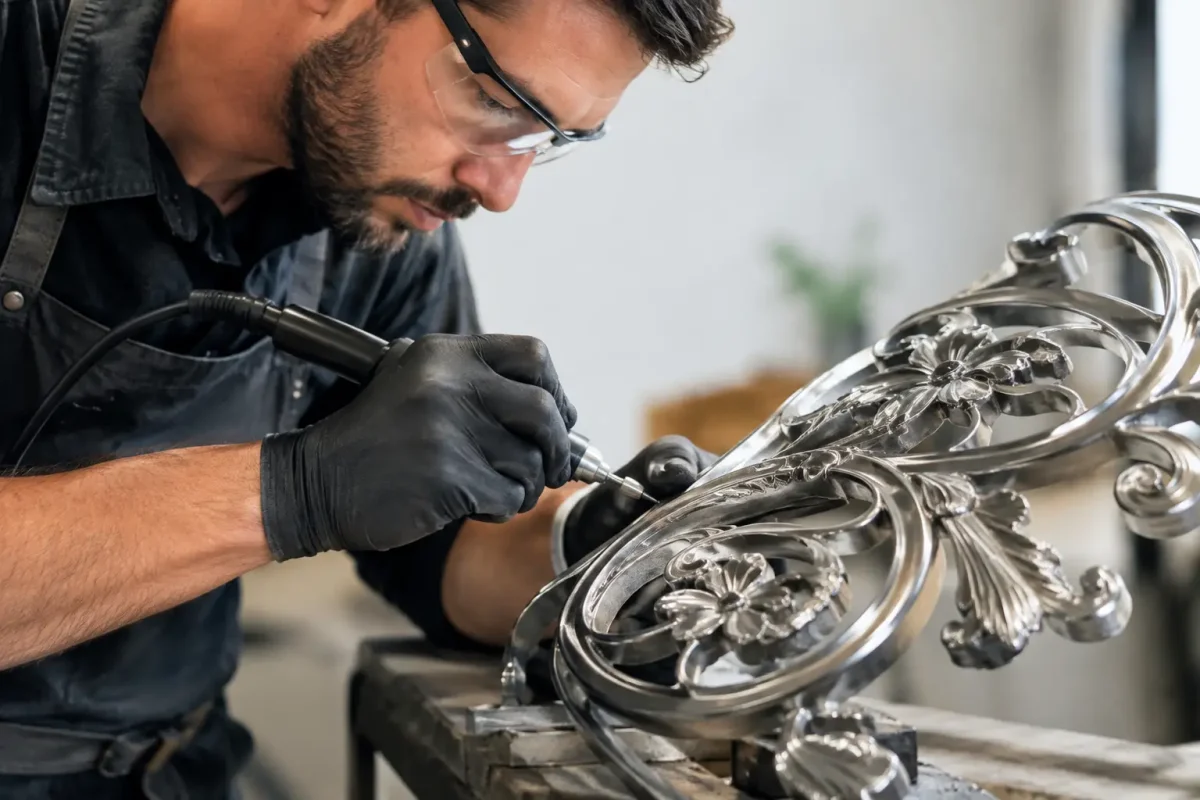
Best Process for Intricate Metalwork Explained

Best Process for Intricate Metalwork Explained

A tight internal radius, a fine decorative lattice or a run of precisely located fixing holes can turn an ordinary profile-cut job into a costly problem. Choose a process that puts too much heat into the sheet and narrow sections may move. Choose one that cannot hold the detail and the finished part may not fit, weld or present as intended. The best process for intricate metalwork is therefore not one machine for every job. It is the process that suits the material, thickness, required edge condition and the purpose of the final component.

For fabricators, builders, manufacturers and designers, the practical choice usually comes down to CNC laser cutting or CNC waterjet cutting. Both produce accurate profiles from a digital drawing. Their strengths are different, and knowing where each process performs best helps protect lead times, material yield and the quality of the parts arriving at your workshop.

Start with the finished part, not the cutting machine

Intricate work is often described by its appearance, but appearance is only part of the specification. A decorative screen with hundreds of small apertures has different requirements from a stainless steel machine guard, even if both have detailed patterns. The screen may prioritise crisp presentation and efficient production. The guard may need precise mounting points, minimal heat effect and a clean edge that is safe to handle.

Before selecting a cutting method, establish the material grade, thickness, overall sheet size and critical dimensions. Consider whether the part will be folded, welded, painted, powder coated, polished or installed with other components. Also identify the smallest features in the drawing: narrow bridges, small holes, sharp inside corners and fine lettering are often where a design succeeds or fails.

Tolerance should be specified where it matters rather than applied blindly across every dimension. This makes the job more economical while ensuring critical locations, such as bolt patterns or mating edges, receive the attention they require. A good cutting partner will also review whether the requested geometry is realistic for the selected material and process before production begins.

When laser cutting is the best process for intricate metalwork

High-definition CNC laser cutting is usually the efficient option for detailed metal profiles where speed, repeatability and a fine kerf matter. A focused laser beam removes material quickly, making it well suited to production runs and parts with numerous holes, slots and contours.

For thinner steel, stainless steel and aluminium, laser cutting can deliver exceptionally crisp detail with a narrow cut width. That narrow kerf supports close nesting, which can reduce waste on costly sheet. It is also valuable where a project needs a large quantity of identical components, from brackets and panels to architectural inserts and precision fabrication parts.

Laser cutting does introduce heat to the cut zone. On many jobs this is entirely acceptable, particularly when the component is going straight into fabrication or coating. Yet heat can be a deciding factor on intricate profiles with long, narrow sections, sensitive finishes or material that must stay especially flat. Depending on the metal, thickness and design, localised heat may leave a heat-affected edge or create movement that requires further attention.

This does not make laser the lesser choice. It means the drawing and material need to be assessed honestly. If the priority is fast, accurate production of detailed sheet-metal parts, laser is frequently the most practical answer. If preserving the original material condition is non-negotiable, waterjet may be the stronger option.

Design details that suit laser cutting

Laser performs particularly well when small details are repeated across many parts and the material is within a thickness range suited to efficient laser processing. Clean contours, consistent slot widths and sensible spacing between cut features allow the machine to maintain speed and quality.

Avoid designing extremely thin tabs or fragile internal pieces without discussing the part’s purpose first. A feature may be possible to cut but still be vulnerable when the sheet is lifted, transported or handled during fabrication. Practical design support at this stage can prevent a part being technically accurate yet difficult to use.

Why waterjet earns its place on difficult materials

CNC waterjet cutting uses a high-pressure stream of water, with abrasive added for metal cutting, to erode the material along the programmed path. At pressures up to 60,000 PSI, it can accurately cut steel, stainless steel, aluminium and a broad range of other materials without introducing a heat-affected zone.

That cold-cut capability is the major advantage. Waterjet cutting helps retain material integrity where heat distortion, hardened edges or discolouration would create problems downstream. It is a strong choice for intricate metalwork in thicker plate, heat-sensitive materials, highly finished metals and parts that require detailed geometry without thermal effects.

Waterjet also offers valuable versatility when a project includes more than metal. A single cutting method can be used for materials such as rubber, foam, tile, timber and gasket material, allowing related components to be produced with consistent digital accuracy. For businesses managing mixed-material assemblies or prototypes, that flexibility can simplify production planning.

The trade-off is speed. Waterjet is generally slower than laser on thin sheet, especially where a high volume of small features is required. Abrasive cutting parameters, material thickness and edge-quality expectations all affect cycle time. Where fast throughput is the priority and heat is not an issue, laser may offer a better commercial result. Where material preservation and thickness capability lead the specification, waterjet is often worth the additional cutting time.

Edge quality is more than a visual issue

A clean edge affects fit-up, handling and finishing. Laser-cut edges can be very neat, but the result depends on material type, thickness and cutting settings. Waterjet leaves a cold-cut edge and avoids the thermal changes associated with laser cutting, which can be especially useful before welding, machining or polishing.

Neither process removes the need to consider the final finish. Some jobs need light deburring, surface protection or edge treatment after cutting. Planning for this upfront is more reliable than assuming every part will leave the machine ready for immediate installation.

The drawing is part of the manufacturing process

The quality of intricate cutting begins well before the machine starts. A clear vector-based drawing gives the operator the information needed to produce accurate work efficiently. DXF files are commonly suitable for profile cutting, provided they are clean and correctly scaled.

Duplicate lines, open contours, overlapping geometry and dimensions that conflict with the drawing can create delays or unintended cuts. If a pattern includes internal pieces that must remain connected, bridges need to be intentionally designed rather than improvised at the last minute. Likewise, holes positioned close to an edge may need adjustment if the remaining material will be too weak for the application.

For architectural and decorative work, it is also worth checking the pattern at full scale. A motif that looks balanced on a computer screen can lose definition when enlarged across a gate panel or screen. For engineering work, confirm the datum points and any dimensions that must align with existing assemblies. This is where a cutting service adds value beyond simply following a file.

A practical selection method for your next job

The most reliable process choice can be made by working through four questions: What is the material? How thick is it? What is the smallest critical feature? What must happen to the part after cutting?

If you are cutting thin metal sheets in quantity and need fast, sharp detail, laser cutting is likely to the efficient option. If the material is thick, heat sensitive, difficult to cut conventionally or must remain free of heat distortion, waterjet cutting is likely the better fit. If the job combines several materials or includes precision gaskets, inserts and metal plates, waterjet’s range may reduce the need to coordinate multiple suppliers.

Cost should be measured across the finished job, not only by the cutting rate. A lower initial cutting price can be offset by extra straightening, grinding, rework or rejected material. Conversely, specifying waterjet for a straightforward thin-sheet production run may add time and cost without creating a meaningful benefit. The right decision is the one that achieves the required quality with the least downstream disruption.

Local capability makes process selection easier

Having both technologies available in one Adelaide workshop removes the pressure to force every project through a single machine. Waterjet & Laser SA can assess the drawing, material and end use, then recommend the process that best suits the job rather than the equipment that happens to be available.

That is particularly useful when deadlines are tight or the design is new. A small review before cutting can identify fragile features, improve sheet use, confirm realistic tolerances and select a process that supports the intended finish. It is a practical step that saves time once fabrication is underway.

The best results in intricate metalwork come from treating cutting as an engineering decision, not a commodity purchase. Bring the intended outcome, the material details and a clean drawing to the conversation, and the right process can turn a complex pattern into dependable, production-ready parts.

How to Specify Gasket Dimensions Accurately

How to Specify Gasket Dimensions Accurately

A gasket can look like a simple ring, yet a 1 mm discrepancy at the bore, bolt pattern or sealing land can stop a flange from sealing properly. When a part is being cut for an urgent shutdown, a pump rebuild or a production run, the drawing needs to remove guesswork before material reaches the cutting bed. Knowing how to specify gasket dimensions clearly helps deliver parts that fit first time and perform as intended.

Start with the real sealing requirement

Before measuring an old gasket or drawing a profile, identify what the gasket must seal. The flange arrangement, operating pressure, temperature, medium and bolt load all influence the suitable profile and material. A gasket for a low-pressure water connection may need very different allowances from one used around oils, chemicals, compressed air or abrasive slurry.

The sealing face is the starting point, not the worn or distorted gasket removed from service. Old gaskets can compress, stretch, tear during removal or swell after exposure to fluid. They are useful as a reference, but should not be the only source of dimensions where accuracy matters.

If the mating parts are available, measure the flange faces directly. Confirm whether the gasket sits inside the bolt circle, outside it, within a recess, or over a raised face. Also check that the gasket’s inside edge will not project into the flow path. Material protruding into a pipe or pump bore can create turbulence, wear and contamination issues.

How to specify gasket dimensions from the sealing face

For a standard circular gasket, provide the inside diameter, outside diameter and finished thickness. These dimensions should be stated in millimetres and labelled clearly as ID, OD and thickness. Do not rely on a note such as “suit 100 NB flange” alone. Nominal pipe and flange sizes are useful references, but standards vary and they do not always describe the exact sealing arrangement in front of you.

The ID should suit the open bore or the required clearance around it. The OD should sit fully on the available sealing land without extending beyond the flange edge or interfering with bolts. Where a gasket must locate in a groove or recess, specify the groove dimensions as well as the gasket dimensions, and state any desired clearance.

Thickness requires more consideration than it first appears. A thicker gasket can accommodate some irregularity in mating faces, but it may require more bolt load and can be more prone to extrusion in demanding applications. A thinner gasket may offer better stability, provided the flange faces are suitably flat and the material is appropriate. Specify the actual finished thickness required, rather than describing it only as “thin” or “heavy-duty”.

For non-round profiles, dimension the overall length and width, then identify every internal opening, corner radius, slot and tab that affects fit-up. Give dimensions from consistent datums, such as the horizontal and vertical centre lines, rather than chain-dimensioning features from one another. This approach prevents small measurement differences accumulating across the part.

Define bolt holes and alignment features

Bolt holes are among the most common causes of unusable gaskets. State the quantity of holes, their diameter and their position. For equally spaced holes, provide the pitch circle diameter, number of holes and angular orientation. The orientation matters whenever there is a non-symmetrical feature, such as an offset port, a single locating hole or an irregular outer profile.

For example, a complete instruction may read: “Eight 14 mm holes equally spaced on a 180 mm PCD, with one hole centred on the vertical centre line.” That tells the cutter where the pattern starts as well as how it is distributed.

Slotted holes need their width, overall length, end radius and orientation. If a slot is intended to accommodate installation variation, make that clear. A slot deliberately added for tolerance is different from a slot that forms part of the seal boundary.

Where a gasket includes multiple ports, label each one on the drawing. Similar-looking openings can have different purposes, and a rotated part may not become apparent until installation. A clear “TOP”, “FLOW END” or orientation mark can prevent expensive delays on site.

Set tolerances that suit the job

Every cut part has manufacturing variation, and every application has a practical limit for that variation. Specifying unnecessarily tight tolerances can increase cost and lead time without improving the seal. Leaving tolerances undefined can create avoidable ambiguity.

The right tolerance depends on gasket size, material, thickness, flange design and the consequences of misalignment. A large rubber flange gasket may function well with a more practical tolerance than a small multi-port gasket for precision equipment. Critical dimensions are usually the ID, bolt-hole locations, narrow sealing lands, internal ports and any locating features.

State general tolerances where appropriate, then call out tighter requirements only on critical features. If you are matching a supplied component, include its measured dimensions or provide the component for checking. For repeat production, an approved sample can be valuable because it establishes a physical benchmark alongside the drawing.

Keep in mind that flexible materials behave differently from steel. Rubber and foam can move slightly during handling, while fibre sheet materials may have grain direction or edge characteristics that affect performance. Dimensions are normally specified in the free, uncompressed state unless the drawing says otherwise.

Specify the material, not just the shape

Two gaskets with identical dimensions can perform very differently. The cutting specification should identify the material grade or type, thickness and, where relevant, hardness. If the exact product is known, provide the manufacturer’s material designation. If it is not known, provide the service conditions so an appropriate option can be discussed.

Useful information includes the fluid or gas being sealed, maximum operating temperature, pressure, exposure to weather or UV, and whether food-grade, chemical-resistant or electrical-insulation properties are required. For rubber materials, Shore hardness can be relevant. For compressed fibre, graphite or other specialised sheets, the intended application matters just as much as the profile.

Material selection and dimensioning are connected. A soft, compressible material may need different bolt-hole clearance from a stiffer sheet. A gasket exposed to chemicals may change size in service, so the material’s compatibility should be confirmed before finalising the profile.

Supply a drawing that can be cut accurately

A dimensioned PDF is often enough for a straightforward gasket, provided it includes all critical measurements, material details, quantity and revision number. For intricate parts, a DXF or DWG file is preferable because it gives the cutter a direct profile to review. A scale drawing without dimensions is not a reliable manufacturing instruction, as print settings and imported geometry can change size.

Check the CAD file before sending it. Confirm it is drawn at 1:1 scale in millimetres, contains only the required cut lines, and does not include duplicate lines or hidden geometry. Closed profiles are particularly important. An unclosed line can cause an incomplete cut or introduce uncertainty about the intended edge.

If you are working from a hand sketch, make it legible and include a photograph of the mating flange with a tape measure where useful. A sketch does not need to be elaborate. It does need to establish the shape, dimensions, hole pattern, material and orientation without conflicting notes.

Choose the cutting process around the material

Waterjet cutting is particularly well suited to rubber, foam, fibre gasket sheet and other materials that should not be exposed to heat. The cold-cut process avoids heat distortion and can produce detailed profiles, small holes and intricate internal features. It is also useful where material integrity at the cut edge is a priority.

Laser cutting can be an efficient option for suitable materials and applications, particularly where speed and clean profile cutting are required. The best process depends on the gasket material, thickness, edge requirement, part complexity and quantity. For gaskets, the material should guide the process choice rather than simply selecting the fastest available machine.

At Waterjet & Laser SA, supplying the drawing and the application details together allows the cutting method, nesting and tolerances to be checked before production. That reduces the risk of a technically accurate profile being cut from a material that is unsuitable for the job.

Checking gasket dimensions before cutting

A final pre-cut review is worthwhile, especially for low-volume custom parts. Compare the drawing against the flange or mating component one more time. Verify ID, OD, thickness, bolt-hole count, PCD, orientation, material and quantity. Check that revision numbers match across the purchase order, drawing and CAD file.

For a first-off part with a complex pattern, a simple paper print at full scale can reveal errors quickly. Place it over the flange and check ports, bolts and outside edges. This small step is often faster than correcting a batch after cutting.

Clear gasket specifications do more than produce a neat profile. They protect sealing performance, installation time and project schedules. When the dimensions are measured from the real sealing arrangement and communicated with the material and tolerances in mind, the finished gasket has the best chance of doing its quiet but essential job properly.

When Outsourced CNC Cutting Makes Business Sense

When Outsourced CNC Cutting Makes Business Sense

A fabrication job can stall over one missing bracket, a run of inaccurate profiles or material that has distorted during cutting. Outsourced CNC cutting gives businesses a practical way to keep work moving without taking on the cost, maintenance and operator requirements of running specialist equipment in-house. For Adelaide fabricators, builders, manufacturers and designers, the value is not simply access to a machine. It is access to the right process, dependable capacity and parts ready for the next stage of production.

When outsourced CNC cutting is the better option

Buying CNC cutting equipment can make sense for businesses with a consistent, high-volume workload in a narrow range of materials. But the real investment is much larger than the machine itself. There is programming, consumables, maintenance, extraction or abrasive handling, training, floor space and the cost of downtime when a critical component fails.

Outsourcing is often the stronger option when demand changes from week to week, when a job requires materials outside your usual capability, or when your own workshop is already at capacity. It allows a business to take on work with confidence without tying up capital in equipment that may sit idle between projects.

This is particularly useful for fabrication shops balancing urgent repair work with scheduled production. Rather than delaying a customer job while profiles are cut manually, a contractor can send through a drawing and receive accurately cut parts that are ready to fold, weld, machine, assemble or install. The same approach suits architectural metalwork, signage, automotive components, mining repairs, gaskets, flooring details and one-off custom designs.

Outsourcing also reduces the risk of choosing a process that does not suit the material. A clean cut in thin stainless steel may call for laser cutting, while a thick aluminium plate, rubber gasket or tile detail may be better suited to waterjet. Having both capabilities available from one supplier removes unnecessary compromise.

Outsourced CNC cutting is about process selection

CNC cutting is not one service with one result. The cutting method affects edge quality, speed, heat input, material condition and overall cost. A supplier that understands the differences can help you make a practical choice before material is loaded onto the machine.

When laser cutting is the efficient choice

High-definition CNC laser cutting is generally a fast and accurate option for many metal profiles, particularly sheet steel, stainless steel and aluminium. It is well suited to production runs, repeatable parts and detailed profiles where fast processing matters. Clean edges can reduce finishing time and help fabrication teams move quickly into folding or welding.

Laser cutting uses heat, so the result depends on material type, thickness and part geometry. On some applications, a heat-affected zone is acceptable or insignificant. On others, it may not be suitable. Parts with very fine features, tight nesting requirements or demanding cosmetic finishes should be discussed before production so the right settings and process are selected.

When waterjet is the smarter choice

Waterjet cutting uses a high-pressure stream of water, often mixed with abrasive, to cut material without a heat-affected zone. Waterjet & Laser SA operates waterjet technology at pressures of up to 60,000 PSI, delivering precision cutting while preserving the material characteristics around the cut edge.

That cold-cut process is valuable when heat distortion, hardening or discolouration could create problems later. It is also exceptionally versatile. Steel, stainless steel, aluminium, rubber, foam, gaskets, tiles, pavers, timber and many other materials can be profile cut with waterjet technology.

Waterjet may take longer than laser on certain thin metal jobs, so it is not automatically the lowest-cost choice. Its advantage lies in material versatility, thickness capability and the ability to cut intricate shapes without thermal stress. For a project involving mixed materials or sensitive finishes, that trade-off can save time and waste further down the line.

What to provide for an accurate quote and clean result

Good outsourced work begins well before the cutting starts. A clear drawing and accurate material information help prevent delays, incorrect assumptions and unnecessary rework. DXF files are commonly preferred for CNC profile cutting because they provide usable geometry, but a PDF drawing with dimensions can also be useful for reviewing the job.

Specify the material, thickness, quantity and whether you are supplying the sheet or require material supplied. Include any critical dimensions, hole sizes, bend allowances, grain direction, surface-finish requirements and deadlines. If the finished part will mate with another component, say so. A cut profile that looks correct on a drawing can still cause assembly issues if tolerances, tabs or kerf considerations have not been allowed for.

It is also worth identifying what happens after cutting. A part that will be powder coated, galvanised, welded or machined may need different allowances than a decorative panel that will be installed as-cut. For architectural screens, detail can be both a design feature and a manufacturing challenge. Fine bridges, narrow sections and very small internal cut-outs need to be reviewed against the material thickness and intended use.

The most efficient suppliers will raise these questions early. That is not a delay in the process. It is how costly surprises are avoided when a job reaches fabrication or site installation.

Capacity without sacrificing quality control

Outsourcing should not mean giving up control over the quality of your parts. It should mean gaining a specialist production partner with the equipment and experience to produce repeatable results. Before committing to a supplier, assess more than the quoted price.

Ask whether they can cut the specific material and thickness required, whether laser and waterjet options are available, and how they manage urgent work. Consider their communication during quoting as well. If a drawing is unclear or a process is unsuitable, a capable supplier should explain the issue directly rather than proceed with a guess.

Turnaround also needs to be viewed realistically. A quick cut is only useful if the order is correct, packed properly and available when your team needs it. For businesses working across Adelaide, regional South Australia and interstate projects, reliable delivery arrangements can be as important as cutting speed. A delayed part can leave welders, installers and site crews waiting.

For repeat work, retain approved drawings, revision details and material specifications. This makes reordering faster and reduces the chance of an older version being cut by mistake. It also gives the cutting provider a clearer basis for maintaining consistency across batches.

Using outsourced capacity to win better work

There is a commercial advantage to having specialist cutting capacity behind your business. A builder can quote detailed steelwork without purchasing cutting machinery. A fabricator can accept an overflow job rather than turn it away. A designer can specify complex patterns in metal, tile or timber with confidence that the idea can be manufactured accurately.

The key is to quote responsibly. Allow enough time for drawing review, material sourcing, cutting and any secondary fabrication. Do not assume every material behaves the same way, and do not base a decision solely on the cheapest per-part rate. Edge condition, material integrity, nesting efficiency and turnaround can all affect the actual cost of completing the job.

When outsourced CNC cutting is treated as part of the production plan rather than a last-minute fix, it creates room to take on more specialised work while keeping your own workshop focused on its best skills. Send clear information early, choose the process that suits the material, and let accurate cutting set the standard for everything that follows.

Secret Link